Top Conveyor Equipment Manufacturers Worldwide
Conveyor systems quietly shape modern production, warehouses, ports, and distribution centers. They move cartons, pallets, parcels, and bulk materials through controlled routes. According to MarketsandMarkets, the global conveyor system market could grow from approximately USD 7.2 billion in 2023 to USD 9.5 billion by 2028. The report identifies automation, e-commerce fulfillment, and manufacturing expansion as major growth drivers. Grand View Research also reports steady market growth through 2030, although estimates differ because research firms use different product and regional definitions.
This guide examines the top Conveyor Equipment manufacturers worldwide through practical and technical criteria. These include product reliability, engineering capability, throughput, energy use, customization, maintenance access, and after-sales support. A strong supplier should explain belt width, load capacity, transfer speed, motor efficiency, and emergency-stop design clearly. It should also provide credible testing records and installation guidance. Small details matter. A poorly aligned roller can damage packages, increase noise, and stop a production line.
Not every large company performs equally well in every application. That matters. A supplier experienced in airport baggage handling may not suit a dusty cement plant. Market rankings can also oversimplify real performance. Therefore, this overview combines published industry data with application-focused evaluation. It considers global reputation, manufacturing experience, technology development, service coverage, and customer value. Readers should still verify local support, spare-part availability, operating conditions, and total ownership costs before making a final decision.
What Conveyor Equipment Manufacturers Produce and How They Are Classified
Top Conveyor Equipment Manufacturers Worldwide
What Conveyor Equipment Manufacturers Produce and How They Are Classified
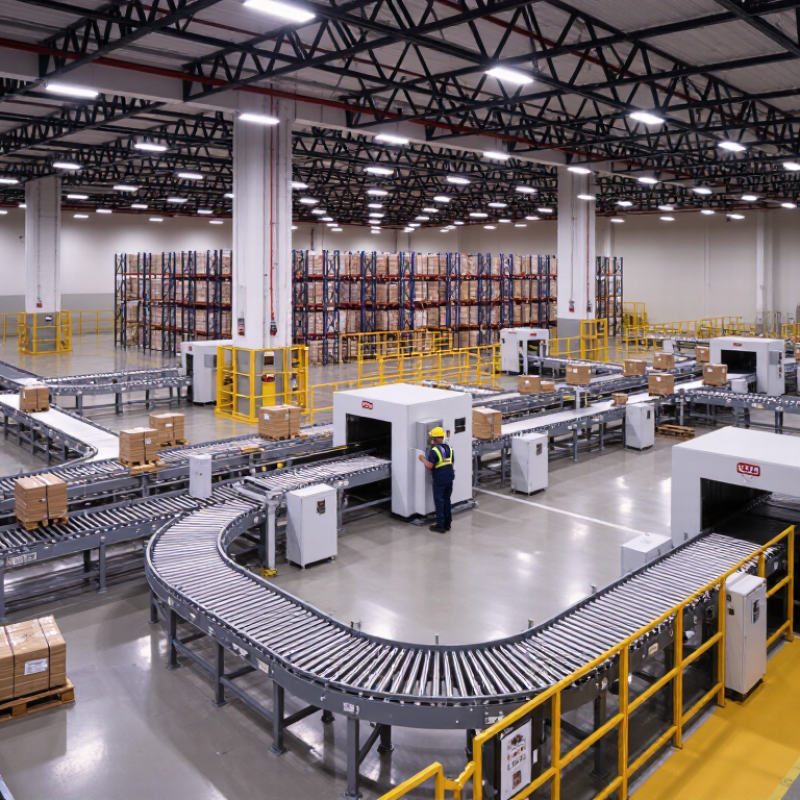
Conveyor equipment manufacturers produce complete material-handling systems, individual machines, and replacement components. Their products may include belt conveyors, roller conveyors, chain conveyors, screw conveyors, feeders, lifts, sorters, and transfer units. They also build frames, pulleys, rollers, motors, guards, sensors, and control panels. These details matter because a small alignment error can increase noise, friction, and maintenance needs.
Manufacturers are commonly classified by conveyor design, conveyed material, and operating purpose. Belt systems suit packaged goods and bulk materials. Roller systems support cartons, pallets, and containers. Chain conveyors handle heavier loads, while screw conveyors move powders or granular materials through enclosed channels. Some suppliers focus on warehouse automation. Others serve food processing, mining, recycling, or agricultural operations. Their engineering teams usually provide layout planning, load calculations, safety testing, installation support, and maintenance guidance.
Classification is not always clean. A hybrid line may combine belts, rollers, scanners, and robotic transfers. Real sites also expose weaknesses that brochures rarely mention, including dust buildup, uneven loading, and difficult access around motors. Reliable manufacturers study these conditions before selecting equipment. They should explain capacity, speed, noise, cleaning requirements, energy use, and expected service intervals in practical terms. Buyers should question vague performance claims and request test data where possible. The best design is not always the fastest one. It may be the system workers can inspect safely and maintain without unnecessary downtime.
Key Technologies Used in Modern Conveyor Equipment
Modern conveyor equipment is becoming a connected production system, not a simple belt and motor. Variable-frequency drives adjust speed smoothly, reducing product damage and unnecessary energy use. Photoelectric sensors detect gaps, jams, and misplaced cartons within milliseconds. Programmable logic controllers then coordinate motors, diverters, and emergency stops. In commissioning work, small sensor alignment errors often cause larger delays than expected.
Condition-monitoring sensors add another layer. They track bearing temperature, vibration, belt tension, and motor current. Maintenance teams can identify abnormal patterns before a conveyor stops. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023, showing the wider shift toward automated material flow. MHI’s 2023 Annual Industry Report also found that 83% of supply-chain professionals expected technology investment to increase over the following five years. However, automation data is only useful when operators trust it and respond quickly.
Tips: Use edge monitoring for fast alarms, but store selected data for long-term analysis. Test safety circuits under real load conditions. Keep manual override procedures visible. Vision systems can improve sorting accuracy, yet poor lighting still creates false readings. Digital twins help model throughput, although their predictions may miss dust, worn belts, or irregular packages. The best design combines software intelligence with practical inspections.
How to Compare Leading Conveyor Equipment Manufacturers
Top Conveyor Equipment Manufacturers Worldwide
Comparing leading conveyor equipment manufacturers requires more than checking purchase price. The right assessment begins with load, layout, speed, sanitation, and maintenance access. A supplier experienced with carton lines may perform poorly on abrasive bulk materials. Ask for operating references from facilities with similar duty cycles.
Market data provides useful context. Grand View Research estimated the global conveyor system market at approximately USD 10.6 billion in 2023, with growth projected through 2030. MarketsandMarkets forecasts continued expansion, driven by warehouse automation, e-commerce, and manufacturing investment. These figures suggest demand is rising, but they do not prove that every manufacturer offers equal value. Report definitions also differ. That matters.
Compare measurable evidence. Request documented throughput tests, energy data, noise readings, and mean time between failures. Review the conveyor’s frame stiffness, belt tracking method, motor efficiency, sensor protection, and spare-parts availability. A three-year service estimate can expose a low initial price. It can also reveal costly downtime.
Ask how the supplier handles commissioning. Slow support hurts.
Strong manufacturers provide drawings, risk assessments, manuals, training, and clear warranty terms. They should explain expected performance under temperature, dust, moisture, and variable loading. One weakness remains common: buyers often compare equipment before mapping actual material flow. That mistake can produce excess transfers, awkward access points, and unnecessary controls. A site visit and a short pilot run usually reveal more than polished brochures. Repair access should be tested physically, not assumed from photographs.
Top Conveyor Equipment Manufacturers Worldwide: How to Compare Leading Suppliers
Conveyor equipment should be compared by operating speed, load requirements, material characteristics, layout, maintenance needs, and application suitability. The chart shows the midpoint of commonly published engineering speed ranges for major conveyor equipment types.
Typical reference ranges: belt conveyors 60–300 m/min, roller conveyors 10–120 m/min, chain conveyors 5–30 m/min, screw conveyors 10–60 m/min, and bucket elevators 30–100 m/min. Actual performance depends on design, material, incline, load, and operating conditions.
Industry Trends Shaping the Future of Conveyor Systems
Conveyor systems are changing from simple transport lines into data-rich, adaptable infrastructure. Grand View Research estimates the global conveyor systems market was worth about US$10 billion in 2023, with continued growth expected through 2030. That expansion reflects stronger demand from e-commerce, food processing, parcel delivery, and automated warehouses.
Automation is moving quickly. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. Conveyors must now communicate with scanners, robotic pickers, warehouse software, and safety controls. MHI’s 2024 Annual Industry Report found that 55% of supply chain leaders planned to adopt robotics and automation within one to two years. For manufacturers, modular designs, predictive maintenance, and real-time monitoring are becoming practical requirements rather than optional upgrades.
Energy efficiency matters too. High-efficiency motors, variable-speed drives, lighter belts, and regenerative braking can reduce power use during long operating hours. Small improvements count. Experience in distribution facilities shows that poorly positioned sensors can create repeated stoppages, even when the conveyor itself is well engineered. Forecasts can mislead. The fastest line is not always the most productive one; uptime, worker safety, maintenance access, and integration quality often determine the real return on investment. Future-ready equipment should also support easy reconfiguration, because product sizes, order volumes, and labor conditions rarely remain stable.